

Operations | Organisation | People | Resources
STAY CONNECTED AND SIGNUP TO RECEIVE INSIGHT updates
Every dollar of the material prosperity we enjoy can find its roots in the industrial revolution and our ability to produce more for less. We came off the farms to work in the factories and delivered unprecedented growth in wealth for our toil.
This is Part 3 of our series on Asset constraint management: Part 1 | Part 2 | Part 3 | Part 4 | Part 5
Dickens gave us the literary view of what those early days were like and Marx had us thinking about how the means of production, distribution and exchange could be put to better effect if it were all owned and run centrally. Thankfully, I live in a country where Marx’s ideas carry little weight. Instead, our commercial and economic systems are deeply grounded in the concept of free enterprise, with unprecedented opportunity of wealth for toil.
People are at liberty to enter into a voluntary exchange between each other for the provision of goods and services that have the intention of delivering additional value and wealth to both parties. In the free market, it means that we have to compete against all comers in the global economy to both persuade and influence our existing customers to remain loyal and to win new ones.
If we have established that there are customers willing to pay us for products or services we wish to offer the market, then the question has to be how we go about producing them. Because we are thinking about production, we’ll ignore for now the work that goes into, in the first place, the marketing and engineering of the product or service—which is better suited to the domain of portfolio, program and project management.
Productive questions
My definition of production is simply the making of goods or services available for use. It is clear, then, that besides the desirability of the product or service itself, the critical factor is how we go about its production. How long will it take to get to the customer? What fixed and variable costs will I incur in doing so? What contribution will I make per unit, and what profit will the product or service add to my business? What penalties will I incur if I cannot deliver against my promise? What premium might I get if I can supply in shorter times than my competitors? How much do I need to invest in plant, equipment and inventory to be a reliable and agile supplier to my customers? How will I ensure that everything I supply is routinely of a quality that satisfies the needs of my client and minimises rework? What kind of learning program do I need to pursue with my team to continuously upgrade their ability to deliver ever better outcomes?
We owe an enormous debt to the pioneers of productivity, from the ‘scientific management’ of Frederick Taylor to Deming’s System of Profound Knowledge and from Taichi Ohno and the Toyota Production System onto the revolution wrought by Eliyahu Goldratt and his Theory of Constraints (TOC).
Ohno gave us the first fundamental principle of Lean in his famous quote: ‘All we are doing is looking at the timeline,’ he said, ‘from the moment the customer gives us an order to the point when we collect the cash. And we are reducing the timeline by reducing the non-value-adding wastes’. I always thought that the simplicity of Ohno’s injunction was akin to golf: get the ball in the hole in as few strokes as possible, or Goldratt’s injunction to make more money now and in the future. Compelling ideas because of their simplicity but requiring high levels of mastery to accomplish.
Below is a diagram of eight different types of waste identified by the Toyota Production System and subsequent development of Lean Manufacturing. In Goldratt’s words, he stood on the shoulder’s of giants to take what his predecessors had accomplished and use his insights from TOC to go further. While eliminating waste is a good start, it’s not the reason you run a business. What you’re there to do is, as mentioned a moment ago, ‘make more money now and in the future’.

There is a fascinating story told of the early days of TOC production software development. There were two significant challenges. First, most of the focus in those early days was in developing software for financial controls. Thus, access was granted to the ops analysts and programmers for minimal amounts of time in the dead of night when everyone else had gone home. Second, the memory available on the processors was tiny, so the pioneers had to enforce certain assumptions about fixed lead times and batch sizes, or else the computer couldn’t calculate the resulting production plan. This rule on batching and lead times became the norm in the development of materials requirements planning (MRP) software.
“Get the ball in the hole in as few strokes as possible”
The consequence of these fixes was an enormous impost on big manufacturing companies, in the form of the massive inventories the algorithms demanded. In a way, it suited them, as their management accounting systems were being run based on absorption costing principles. The more stock you made, the more of your cost base you ‘absorbed’ into it. Work in progress piled up on the shelves and the balance sheet showed them as assets. The only trouble was that much of the resultant product didn’t have a customer. All that production capacity, working capital and physical space were wasted.
All systems have constraints
Along comes Goldratt with his remarkable truth: all systems have constraints—if they didn’t, the output would be infinite. Since no system is capable of producing an infinite output, the theory holds as a valid falsifiable scientific hypothesis. A consequence of this insight was the development of the Five-step FOCUS, Drum Buffer Rope Scheduling and the TOC approach to management accounting called Constraint Accounting. These three innovations in productivity provided a platform to address the systemic issues associated with the complexity of the production environment.
Consultants and improvement practitioners around the world applied these methods and tools across an increasingly diverse array of industries. It turned out there were four basic production shapes—V, A, T, and I—each of which had their particular challenges. It is a testimony to the power of TOC’s approach to production planning and control that it can tailor the general principle to the specific use case. The four main production archetypes are recalled by the letters VATI because of the way the parts flow through the system. Each process looks like one of the letters, traced from bottom to top.
To quote from Eli Schragenheim’s paper in the TOC Handbook (p.201):
Material dependency, resource dependency, convergence points and divergence points are the fundamental elements of a product flow diagram (PFD). Production operations can be classified into families based on which element is the dominant element in the PFD of that particular operation. If divergence is the dominant element, then we have a V plant. If convergence is the dominant element, then we have an A plant. If both divergence and convergence exist (and exist at the same stage, then we have a T plant. If we have neither convergence or divergence, then we have a simple case of resource contention, and the plants are classified as I plants.
It’s essential to know what kind of product flow you are dealing with if you’re looking to optimise production. The way you implement Drum Buffer Rope (DBR) in each case is different. Some quick examples:
V – producing different electrical cables from separate windings and insulation of the same gauge copper wire.
A – the manufacture of an aero engine.
T – the production of a range of cars of the same model, but with different features such as a sunroof and mag wheels.
I – production of alumina in a refinery.
V and A – the overhaul of an aeroplane. The V pulls it apart to get to all the serviceable components, and the A puts it all back together again.
It is beyond the scope of this article to articulate the way you could use DBR in each environment. Still, there is more than enough evidence that this breakthrough in optimising production is, for all practical purposes, universally applicable. If you are in the market for systemic improvement, some further investigation will yield a handsome return.
A critical success factor for the delivery of excellence in production is the constraint accounting framework. At a speech given to an accounting conference, Goldratt once famously declared that ‘accounting is the number one enemy of productivity’. Accountants would like to know what a product costs so they can establish what profit it contributes when that cost is subtracted from the selling price.
To achieve this feat, they add together the material costs of the widget being produced to the product of the minutes and unit cost of the labour that went into making it. The problem is that not all minutes are equal. Saving a minute at the constraint saves a minute for the system as a whole, whereas saving a minute at a non-constraint is a mirage. Optimising production is a function of how the constraint performs, and not the efficiency of the parts.
Work your working capital
The ultimate in optimised production is that you are able to replace a sold product the instant it is bought by a customer. I go to the supermarket and scan my bar of chocolate across the till. Every gear should go into action to send it to replenish the shelf as if an attachment to an email. But most operations don’t do this. Instead, they wait until the retailer has assembled their sales report; they compare that against their own sales report; they wait to run a sales and operations planning meeting and finally they let a production order loose onto the shop floor. Then, they delude themselves about what makes up a minimum production order and what size batch they need to ship to make it economically viable.
Eventually they have a container load to ship and thousands more bars of chocolate have been sold. The system is stuffed with inventory to try and deal with the extended lead time it takes to replace a bar of chocolate.
They would like to avoid the risk of carrying inventory by doing everything they can on a make to order basis. Their customers won’t tolerate the time it would take to go from order to fulfilment, so they come up with very fancy forecasting algorithms to predict how much they should be making to stock. They always get it wrong and end up writing down or scrapping the excess.
The real task at hand is to understand what is reasonable and possible in terms of lead time to replenishment. By Little’s Law, the less lead time we take, the less inventory there will be in the system. Use the insights from TOC and DBR to reduce lead times, increase due date performance, increase throughput and reduce inventory.
Let me leave you with a few questions:
- What shape does production take in your organisation?
- Do you know where your bottleneck is?
- Are you optimising your limited resources around that constraint?
As an executive in charge of production, you need to be a reliable and responsive supplier to your customers. Yet how do you really know what you can promise, by when? You don’t want to be a tyrant demanding impossible feats from your team. But, until you investigate the principles of TOC, you may not know what is reasonable and possible. In the next article in this series, we’ll look at how maintenance can move from a regret cost to a throughput enabler.
This is Part 3 of our series on Asset constraints management.
Part 1: Asset Constraints Management Capabilities
Part 2: Projecting Projects
Part 3: Producing production
Part 4: Maintaining production
Part 5: Controlling contractors
____________________________
What’s next?
The change from standard thinking to Theory of Constraints (TOC) is both profound and exhilarating. To make it both fun and memorable, we use a business simulation we call The Right Stuff Workshop.
We’d love to run it with you. To learn more:
- download the brochure (no email required)
- schedule a call
____________________________

“Know the whole, focus on the constraint.”
____________________________
An AI Enabled Mining and Metals Operating Model
The Shortest Path From Mineral Potential to the Highest Sustainable Cash Flow
A mining investment earns its return through the conversion of mineral potential into dependable cash flow. Every uncertainty, delay and misplaced commitment along that journey affects how much capital is required, how long it remains exposed and what the investment ultimately delivers.
For those who allocate capital, the challenge extends beyond identifying an attractive resource. The acquisition thesis depends on connected decisions across geology, studies, approvals, construction, commissioning, production and closure. Each decision can strengthen the investment case or quietly erode it.
An AI enabled Mining and Metals Operating System connects evidence, reasoning, accountability and execution across that journey. Systems Thinking provides the whole asset perspective. The Theory of Constraints directs attention towards the factor governing value today. AI helps people interpret information, examine alternatives and coordinate the work required to change the outcome.
“Where is the greatest gap between the value this asset could credibly create and the value it is currently on course to deliver?”
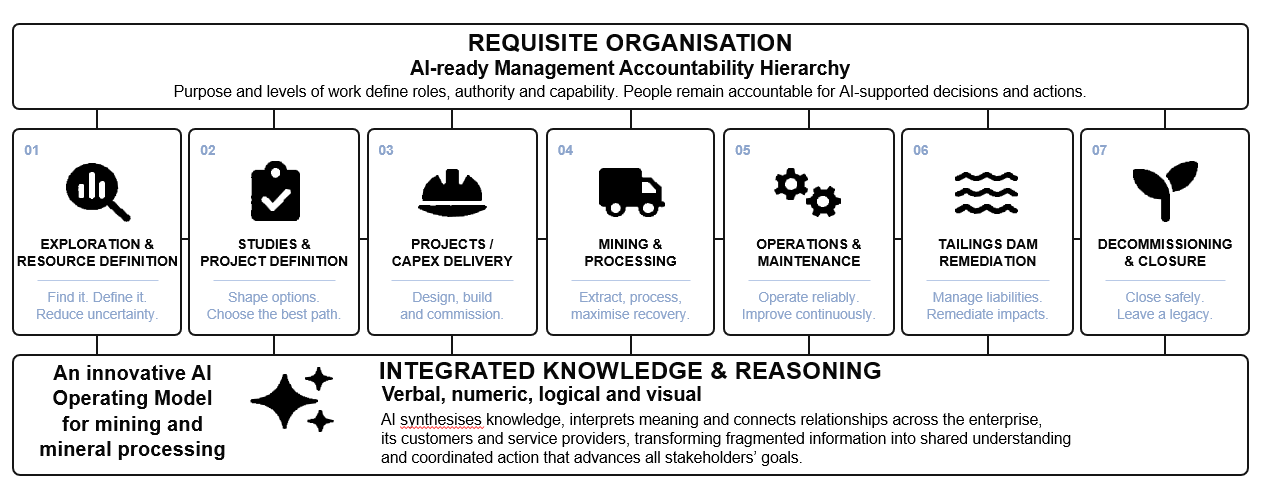
The operating model below brings these ideas together: human accountability above, the life of mine across the centre, and integrated knowledge and reasoning supporting every stage.
Requisite Organisation: put accountability where the work sits
An operating system needs a clear management accountability hierarchy. Purpose and levels of work define the decisions people must make, the authority they require and the capability needed to carry their responsibilities.
A supervisor protecting today’s production, a project director preparing commissioning and a board allocating development capital face different levels of complexity and different time horizons. Each needs information appropriate to the work, clear decision rights and a reliable route for escalation.
AI makes this clarity more important. Recommendations must have accountable human owners, particularly where commitments cross the boundaries between investors, asset owners, contractors and service providers.
For investors, this provides a practical test of execution capability: can the organisation show who owns each assumption in the investment thesis, who can authorise action and how unresolved issues reach the right decision maker?
Exploration and Resource Definition: reduce the uncertainty that matters
Exploration creates value when it resolves uncertainty that changes a worthwhile decision. More data becomes useful when it improves confidence about what is present, where it lies and what further work is justified.
AI can help connect geological reports, assay results, drilling records, geophysical observations and three dimensional interpretations. Shared terminology and traceable relationships allow teams to compare evidence, expose inconsistencies and distinguish observations from interpretations.
The investor’s question is which uncertainty governs the next commitment. A targeted investigation may change the development route, support further drilling or reveal that the opportunity cannot yet justify additional capital.
New sensing and interpretation methods must earn confidence through appropriate validation. The objective is a better sequence of learning and commitment, with uncertainty visible throughout.
Studies and Project Definition: shape options before locking in capital
Studies turn a resource opportunity into choices about mine planning, processing routes, infrastructure, scale and development sequence. Those choices establish much of the future cost, risk and operating flexibility of the asset.
An integrated operating system connects technical narratives, economic models, engineering constraints and spatial representations. Teams can examine whether assumptions agree across disciplines and whether the preferred option remains attractive under plausible changes in conditions.
Approvals, water, power, logistics and workforce requirements belong in this comparison from the outset. Internal experience and relevant external benchmarks can challenge optimistic estimates.
For investors, the benefit is a clearer explanation of why an option deserves funding, what could defeat it and which evidence should be obtained before the next irreversible commitment.
“The most valuable early action may be the one that changes the next capital decision.”
Projects and Capex Delivery: keep the investment case alive
Once capital is committed, the central question becomes whether the project remains on course to deliver its business case. Progress percentages alone cannot answer it.
Engineering maturity, procurement, construction sequencing, approvals and commissioning readiness must be considered together. Individually manageable deviations can combine into a material threat to first production and cash flow.
AI supported delivery intelligence can connect schedules, costs, risks and physical evidence, helping teams identify contradictions and emerging dependencies between formal review gates.
Management can then assess intervention options while choices remain available. A useful assurance process explains what changed, why it matters, who must act and when. Success appears in improved delivery confidence, controlled capital exposure and a credible route into operation.
Mining and Processing: manage the constraint governing saleable output
The economic performance of a mine depends on how extraction, material movement and processing work together. Improving one activity can consume capital without improving the whole.
If processing capacity governs saleable output, increasing mining volumes may simply build stockpiles and working capital. If feed variability constrains recovery, additional plant availability may deliver less benefit than expected.
Connecting mine plans, ore characteristics, plant conditions and production results helps teams investigate these relationships. AI can support the comparison of operating choices, while physical models and simulation help test their consequences.
The discipline is to find the constraint, optimise for it, collaborate around it, uplift it and start again. The measure is the resulting contribution to cash generation, with safety, quality and environmental obligations respected.
Operations and Maintenance: protect the flow of value
Maintenance creates value through its effect on the productive capability of the system. Equipment critical to the governing constraint deserves particular attention because its failure can interrupt the entire flow of output.
An integrated operating system connects procedures, equipment histories, sensor readings, work orders, spare parts and operating conditions. Consistent asset identities and failure classifications help teams interpret information across systems.
AI can support prioritisation and flag emerging patterns for investigation. Simulation can also help operators and maintainers rehearse commissioning, abnormal conditions and recovery from disruption.
For investors, the question is whether this changes reliability and economics: more dependable throughput, better recovery, fewer damaging interruptions and a sustainable balance between production demands and asset capability.
Tailings Dam Remediation: connect obligations with operating decisions
Tailings facilities connect engineering performance, environmental responsibility, operational continuity and long term liability. Their condition and management belong within the investment case.
Inspection reports, monitoring data, risk thresholds, drawings and terrain models can be brought into a shared context. AI can help identify inconsistent records, surface changes requiring attention and connect actions with accountable owners.
Qualified professionals must interpret the evidence and authorise decisions. Traceability matters: the organisation should be able to show what was observed, how it was assessed and what followed.
Where reprocessing or resource recovery is contemplated, the opportunity requires its own technical and economic evidence. Potential value must be considered alongside remediation obligations, additional capital and the consequences of disturbing existing facilities.
Decommissioning and Closure: design the legacy into the economics
Closure decisions begin long before production ends. Land disturbance, infrastructure choices, water management and waste handling can create obligations that persist beyond an investor’s ownership period.
Connecting closure plans with operating and capital decisions helps reveal those consequences earlier. Progressive rehabilitation can be evaluated alongside production needs, while evolving assumptions remain visible in forecasts and decision records.
AI can support the organisation of obligations, evidence and dependencies across the asset’s life. Credible cost estimates and technical judgments remain essential.
For investors, better closure visibility informs valuation, capital planning and exit readiness. A future buyer needs confidence that liabilities are understood, supported by evidence and reflected in the economics.
Integrated Knowledge and Reasoning: connect evidence with action
Supporting every stage is the ability to reason across verbal, numeric, logical and spatial information. Reports explain intent; models quantify consequences; rules establish conditions; drawings and three dimensional models reveal physical relationships.
These sources need shared meaning, or semantics, and explicit relationships, or ontology, within the organisation and across customers and service providers. Otherwise, apparently connected systems can continue to describe different realities.
For example, “ready for commissioning” should connect to agreed requirements for construction completion, inspection, training and operational acceptance.
AI agents can help trace dependencies, identify conflicting assumptions and prepare options. The operating system then connects decisions to owners, scheduled work and completion evidence. Learning from the result updates the next decision.
“Enterprise value is the product. Capabilities are the machinery.”
What’s next?
Begin with one material value problem. Establish the economic baseline and current trajectory. Identify the governing constraint, material uncertainties and credible intervention options. Agree accountable owners, decision gates and a practical action pathway.
Measure the result through time to cash, throughput, recovery, capital exposure, operating cost and liability. Translate changes into the investment model, including implementation costs and avoiding double counting.
An AI enabled Mining and Metals Operating System earns its place when it helps change the asset’s economic trajectory. For investors, the opportunity is a repeatable capability for converting mineral potential into realised value.
Validating medical device concepts before major investment
Concept validation
A concept can look convincing in a presentation and still make an important task harder. A patient may misunderstand an indicator. A clinician may need information the design does not provide. A promising workflow may depend on support unavailable in the intended setting.
These problems become more expensive when the organization discovers them after committing to architecture, tooling or a launch plan.
We must ask how effectively concepts are validated before significant resources are committed. Patient Centered Design treats this as a learning discipline: turn ideas into testable solutions rapidly using low fidelity prototyping, put them in front of relevant users and gather evidence about whether they improve the outcomes that matter.
“A convincing presentation shows what the team hopes will happen. A useful test reveals what people actually do.”
Begin with a question that can change the decision
A prototype without a learning objective can generate interesting comments while leaving the key decision unresolved. Start by identifying what must be true for the concept to succeed.
Does the patient intuitively understand the required action without explanation? Can the professional recognize when the result is ready to use? Does the proposed approach fit the work surrounding the task? Will people take meaningful steps toward adoption?
State the assumption and the evidence needed to assess it. Agree what would support proceeding, what would require revision and what could make the concept unviable. Gather quantitative data along with qualitative verbal feedback.
Prioritize questions with substantial consequences for the investment. An attractive enclosure deserves less attention than an unresolved issue that could prevent safe or practical use of the whole solution.
Choose the simplest useful representation
A picture is worth a thousand words. A simple user experience prototype is worth a thousand pictures. Choose artifacts that maximize learning with the least effort. The appropriate artifact depends on what the team needs to discover.
A sketch may help users explain how they interpret a proposed interaction. A physical mock-up may expose handling difficulties. A simulated interface can support a sequence of tasks. A more complete prototype may be necessary to examine timing, feedback or combined interactions.
Build enough realism to test the assumption accurately. Excessive detail can consume resources without improving the evidence, while insufficient fidelity can conceal the issue being investigated.
Make limitations clear to participants and observers. A manually simulated function may help test an experience, but it does not establish that the technology can deliver that function reliably.
Recruit people who represent the intended use
Patients and healthcare professionals can differ in experience, confidence, physical ability, responsibilities, and access to support. Those differences influence whether the concept helps them complete the job.
Define the participants and contexts relevant to the test. Include people whose circumstances could expose difficulties the development team has overlooked.
A familiar expert may work around a confusing interface that challenges a new user. A clinician from a highly supported center may assume resources unavailable elsewhere. Research needs to reveal these dependencies.
Match the study to its purpose. Exploratory sessions can identify problems and guide iteration. They do not automatically establish population-wide performance or replace the evidence required for later design validation.
Create an Experience Café around real tasks
An Experience Café gives participants a structured opportunity to encounter concepts and talk about their experience. Its value comes from the quality of the scenario, observation and follow-up questions.
Set up situations that reflect what the person is trying to accomplish. Let participants interact with the artifact rather than rely solely on a demonstration by its designer. Build rough and rapid.
Assign roles to facilitators and observers. Agree how comments, actions and difficulties will be captured. Keep the session focused on learning rather than defending the proposed solution. Hold a conversation around the prototype. “Can you show me how you would use this?” “Tell me what you are thinking here.”
Ask participants to explain what they believe is happening and what they would do next. Observe where the concept supports that understanding and where they hesitate, improvise or seek help.
Listen without teaching away the problem
A facilitator can unintentionally make a weak concept appear successful by explaining each step or supplying missing information.
Use neutral prompts and allow participants to reveal their interpretation. When assistance is necessary, record it along with the point at which the person became stuck.
Follow observations with questions about purpose and reasoning. What did the participant expect? Which information did they look for? Why did they choose that action?
Separate a preference from evidence about task performance. “I like this one” may reflect appearance or familiarity. Successful completion, appropriate interpretation and manageable effort provide a stronger basis for assessing whether the concept addresses the need.
“Every explanation the facilitator must supply is a question about what the design expects the user to know.”
Examine the complete experience
The product interaction belongs within a wider job. Test preparation, readiness, execution, monitoring and what follows, wherever these activities affect the concept’s value.
A device may work well once configured while setup introduces avoidable complexity. A result may be easy to view while the professional still needs to transfer it manually before acting.
Include relevant dependencies on caregivers, staff, information and other systems. Investigate whether the concept reduces burden for one participant by increasing it for another.
Use realistic scenarios appropriate to the development stage. Important exceptions and recovery steps deserve attention alongside routine success. An incomplete or interrupted task can reveal weaknesses that a carefully guided demonstration leaves hidden.
Make cognitive burden visible
Ease of use involves what a person must notice, understand, remember, decide and physically do. A tidy interface can still demand substantial mental effort.
Human performance depends on limited attention, working memory and feedback. Examine how the concept supports those processes during a task.
Does it make the relevant information perceptible? Can the user understand its meaning? Is the next action clear? Can they recognize whether that action succeeded?
Look for unnecessary steps, demands to remember information across screens and alerts that interrupt without helping a decision. The best change may simplify a sequence or improve feedback rather than add another feature. Confirm its effect through observation and appropriate measures.
Measure effort alongside task success
Choose measures that reflect the priority outcome and the study’s purpose. These may include completion time, errors, requests for help, repeated actions or failure to notice important information.
Subjective workload measures can complement observed performance. NASA Task Load Index can help structure participants’ assessment of workload, while PURE provides an expert assessment of the effort required to complete tasks. Satisfaction ratings on a Likert scale can be used to compare concepts directly with each other and a baseline solution.
Do not treat one measure as a complete account of usability. Faster completion may accompany misunderstanding. A participant may complete the task correctly while reporting effort that makes repeated use impractical.
Interpret results together and examine the conditions under which they occurred. Record the limitations so decision makers understand what the test has established.
Test demand separately from technical feasibility
Pretotyping examines whether people take meaningful action toward using or adopting an idea before the full solution exists. It addresses a different question from whether a working product can be engineered.
A clearly described concept, service simulation or expression-of-interest process may provide evidence about engagement. The strength of that evidence depends on the action required and the conditions surrounding it.
A click demonstrates less commitment than a substantive implementation conversation. Neither establishes clinical efficacy or successful device use.
For medical concepts, keep representations accurate and make the test status clear. Interpret behavioral evidence alongside clinical appropriateness, access requirements and the responsibilities of the people making adoption decisions. Interest alone cannot establish that the solution should proceed unchanged, particularly when workflows in the clinical setting are involved.
Refine the value proposition with evidence
A value proposition explains which customer the concept serves, the job it supports and the difficulties it intends to reduce. It should connect directly with the outcomes identified through research.
Compare that proposition with the evidence from concept tests. Did participants experience the intended benefit? Did another difficulty become more important? Did the concept require assumptions that the intended setting cannot support? Did the concept do something better than a competitor’s current solution?
Capture both positive and negative findings. Use them to revise the concept, the proposition or the team’s understanding of the need.
Then test the important changes. Iteration should answer a question left open by the previous round. Repeating sessions without changing the artifact or research objective can accumulate comments while leaving uncertainty untouched.
Keep early findings within their proper limits
Early concept validation supports decisions about direction and investment. It does not establish all the evidence needed for a finished medical device.
Technical performance, reliability, clinical benefit and intended-use safety require appropriate subsequent work. A convincing simulated experience may depend on functions the team has not yet demonstrated.
Make these boundaries visible in the decision record. State who participated, what was tested, the conditions, findings and unresolved issues. Explain how those findings affect the next commitment.
Overall, having a “winning concept” in hand, backed by user Experience Café data along with user needs in the form of outcome statements formally structured with a direction of improvement and unit of measure, sets a development team up for success. The outcome statement user needs provide a solid foundation for the design history file.
Rapid prototype experience testing gives the team answers to key decisions and sets a target to pursue early on. This results in faster development cycles, more robust regulatory submissions, and better returns on investment spending.
A Value Management Office can connect this learning with resources and stage decisions. Testing should help the organization commit at a pace justified by evidence and concentrate effort on the uncertainties that govern progress.
“Early validation creates value when it changes the concept or the commitment before an unresolved assumption becomes expensive.”
What comes next
Examine one proposed investment. Which assumption could defeat the concept, and what is the least costly credible way to test it?
Prepare an appropriate artifact, involve representative users and observe meaningful tasks. Review the evidence, revise the concept and record the next learning decision. This gives Patient Centered Design a practical route toward solutions people can successfully use and organizations can responsibly develop.


